PROTEGO®
Pressure and Vacuum Relief Valves with Flame Arrester
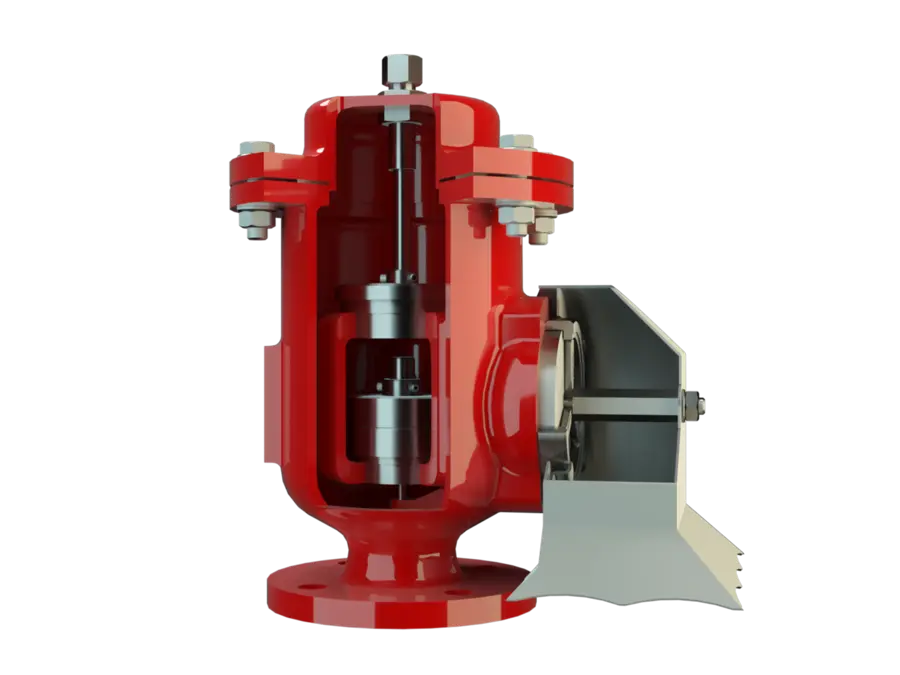
Breather Valves with Integrated Flame Arrester - Emission and Explosion Protection
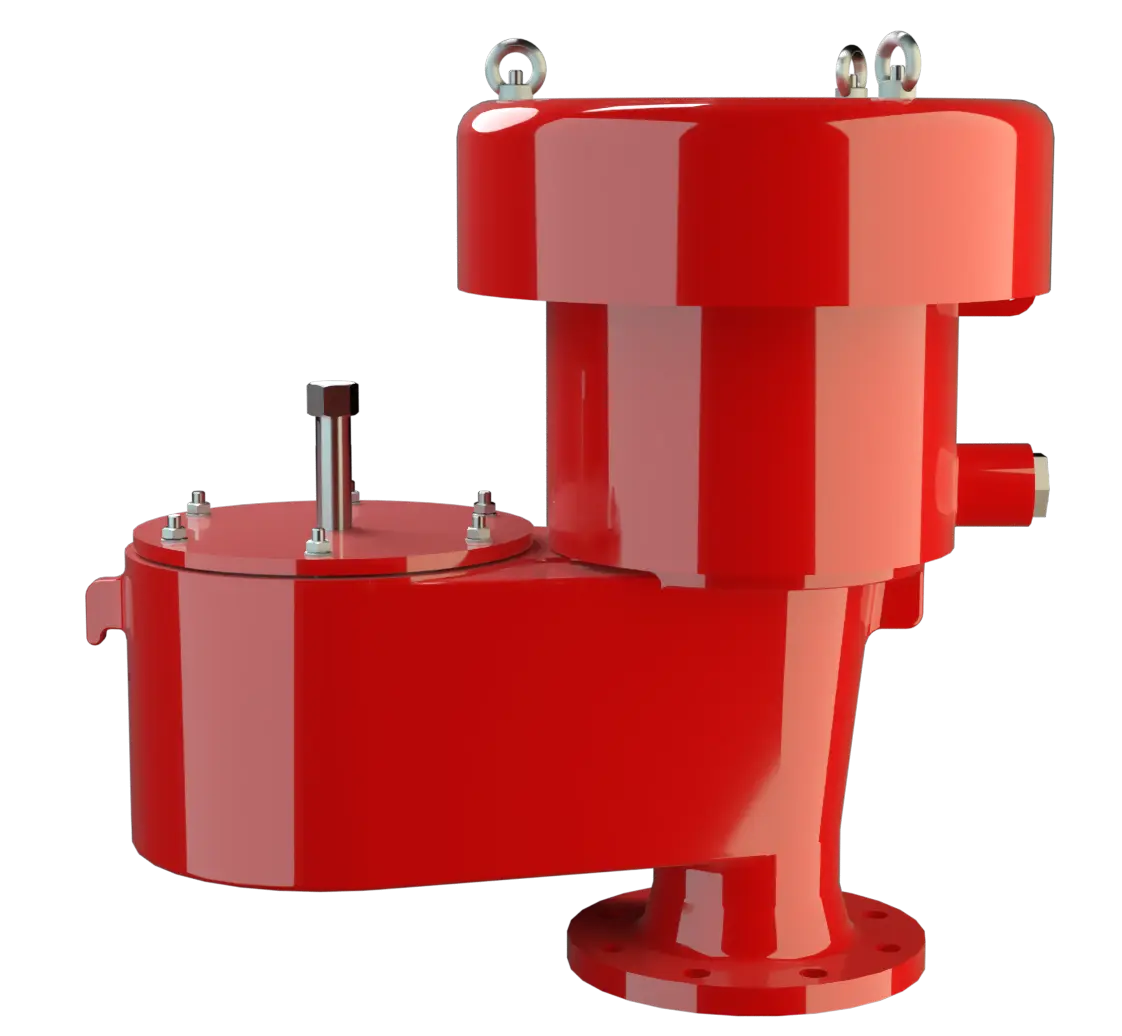
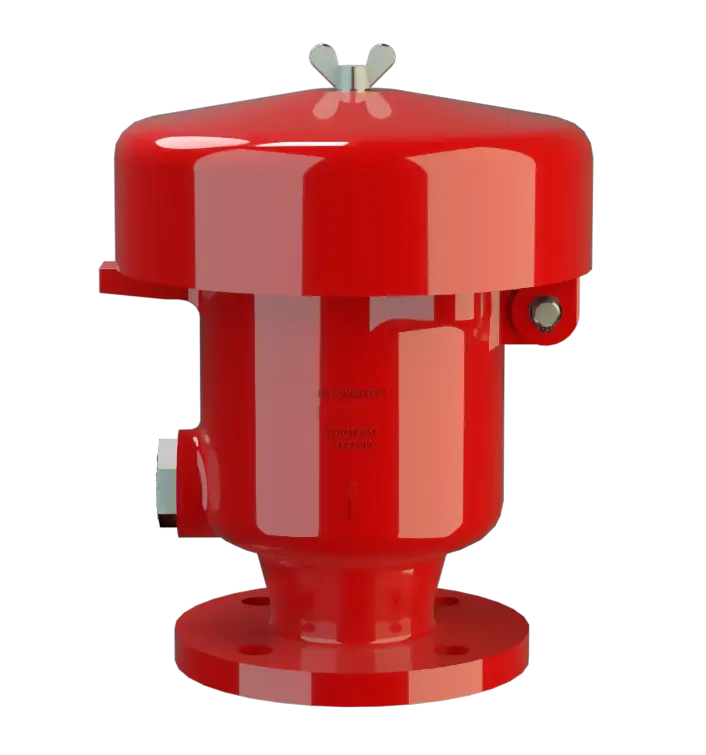
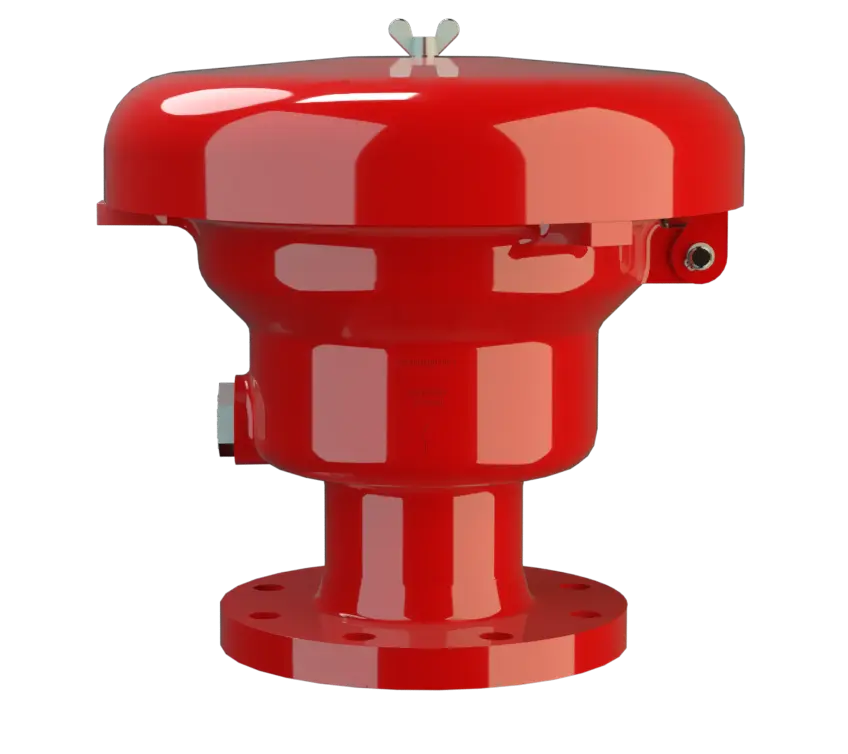
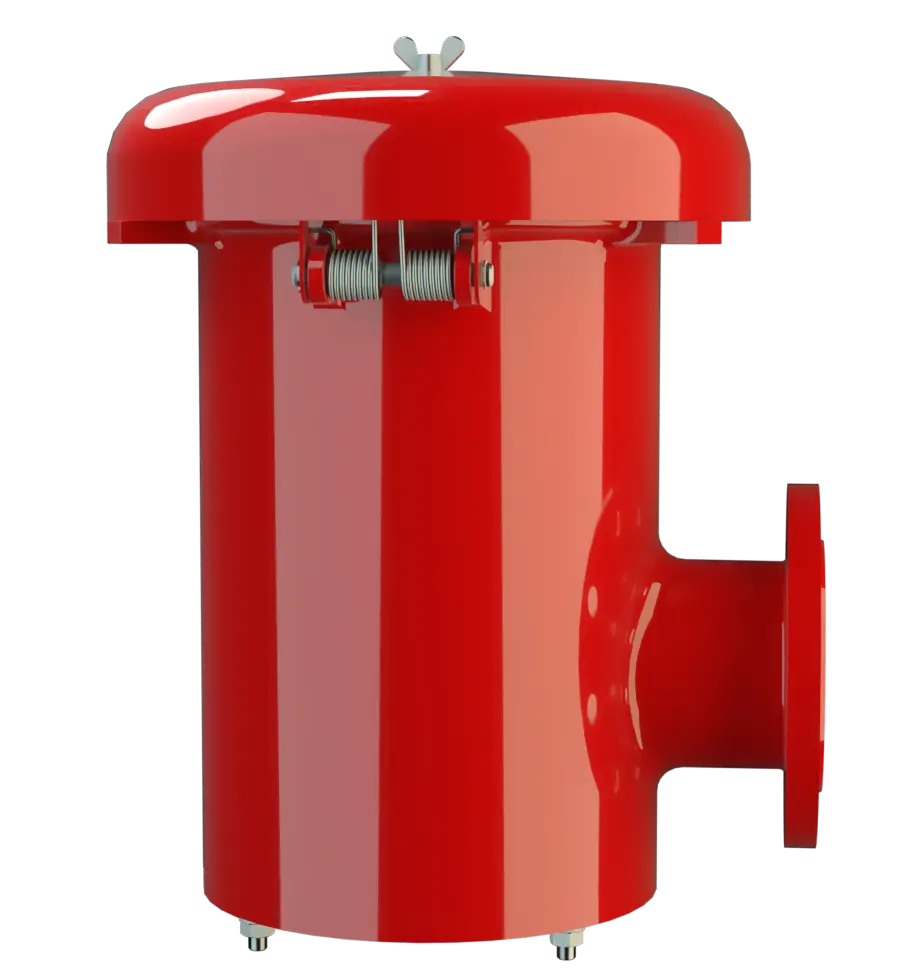
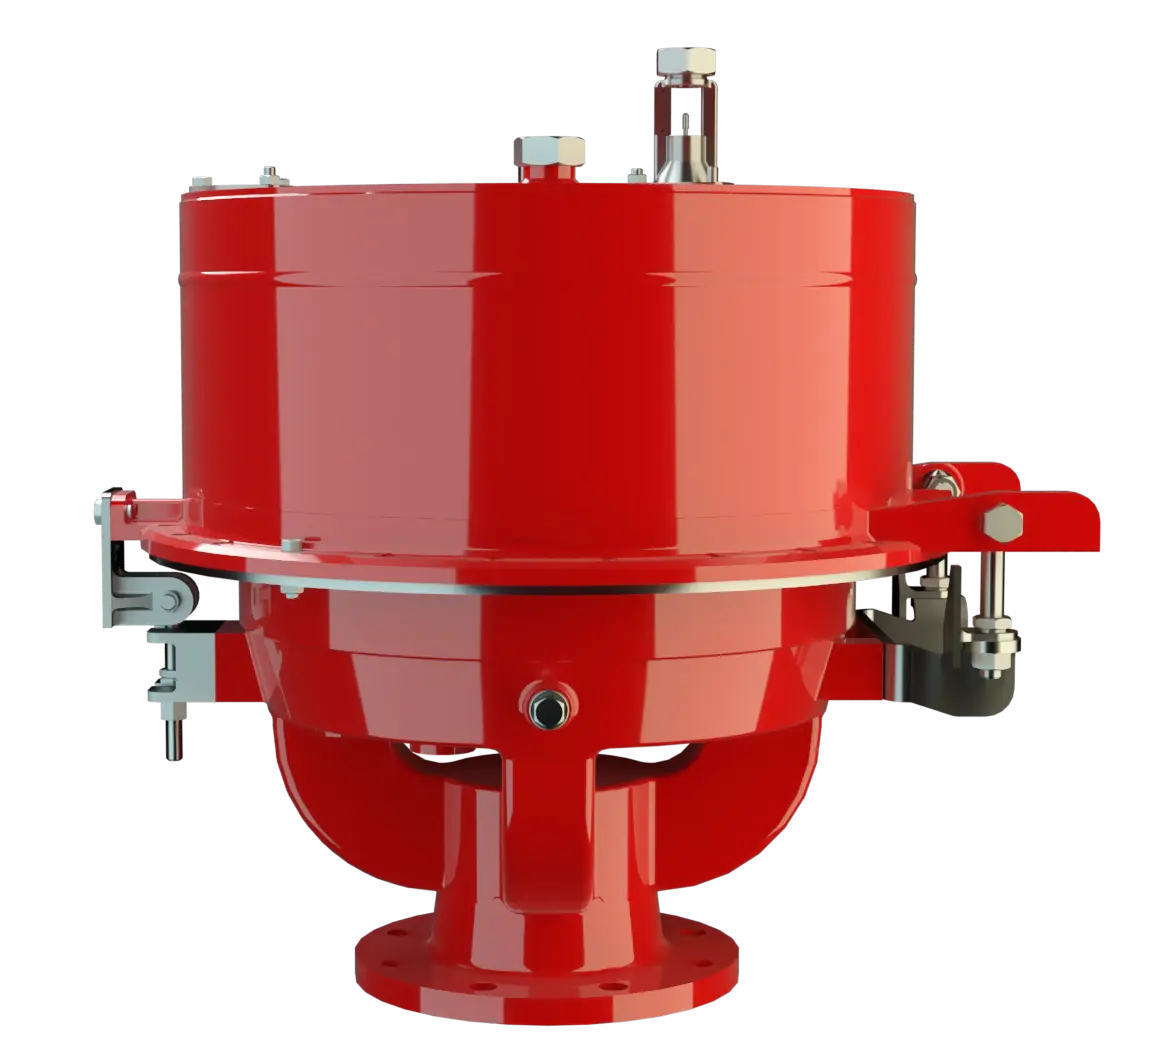
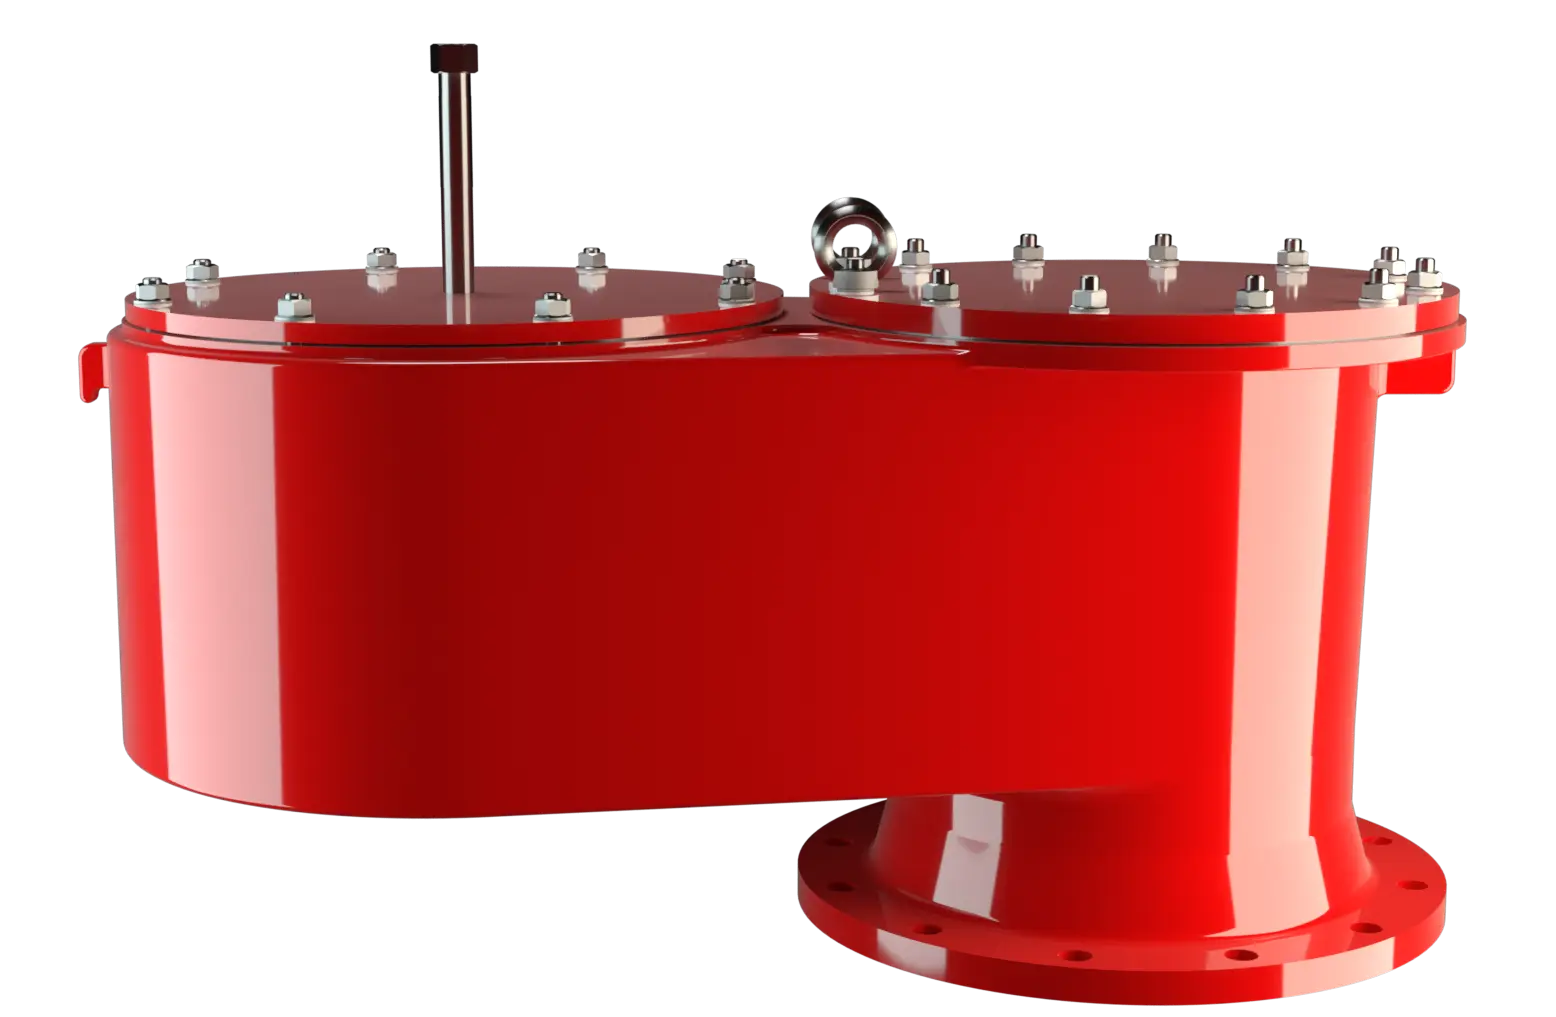
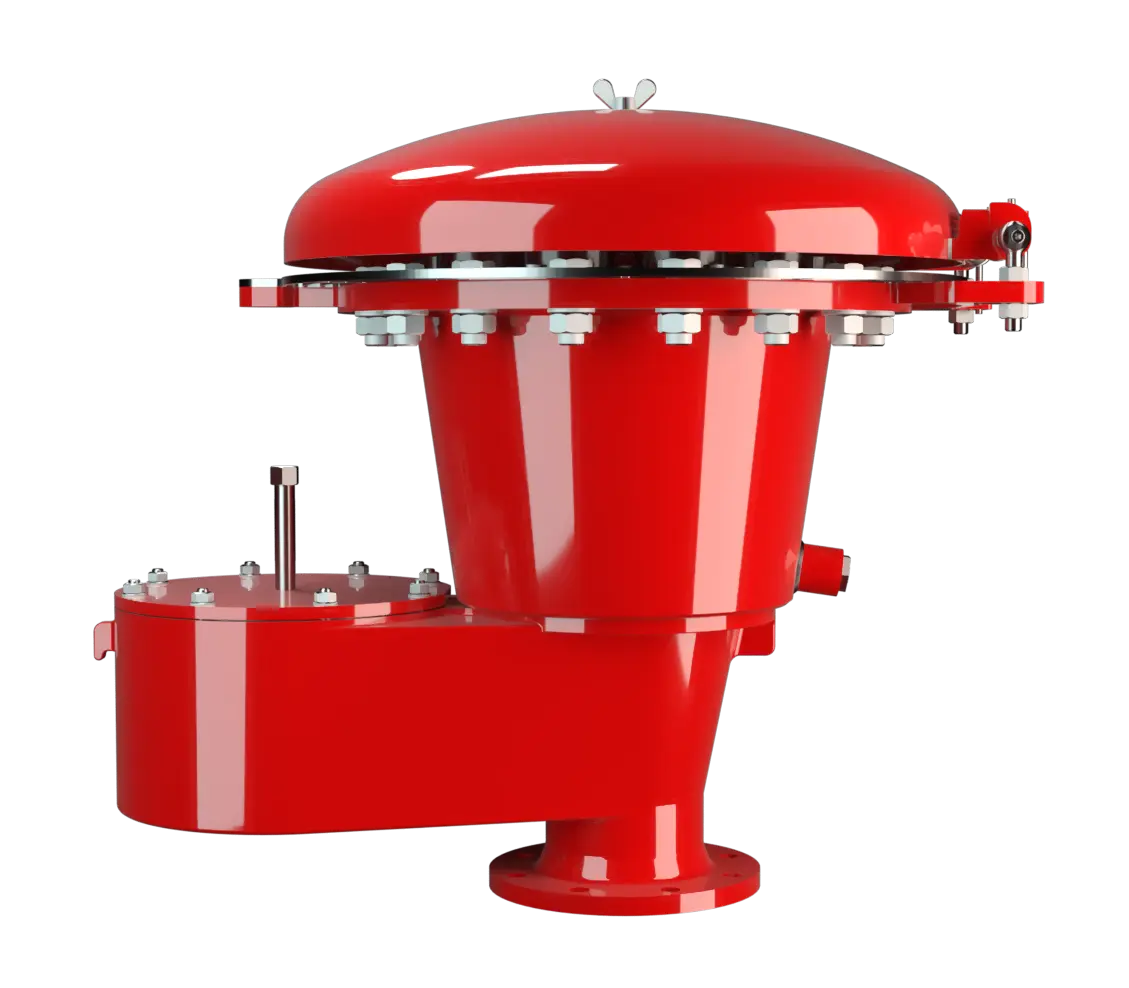
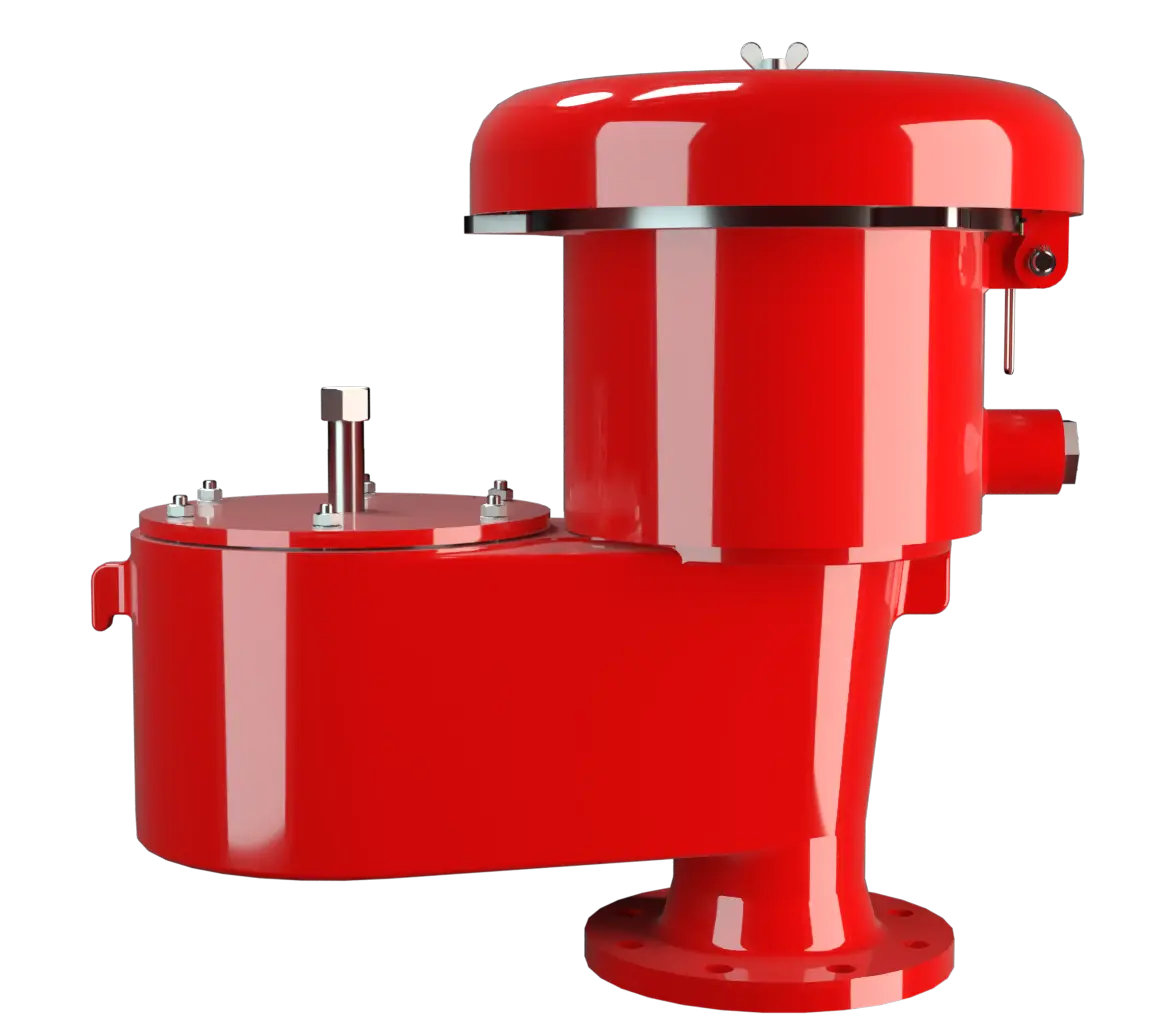
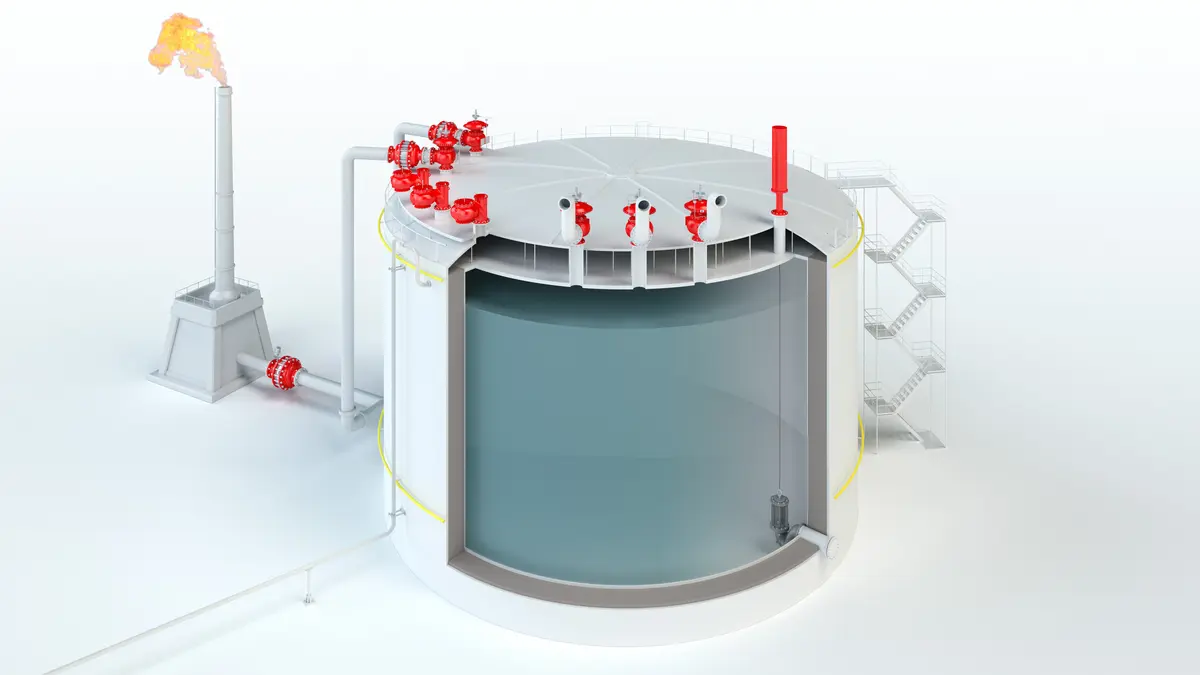
Pressure and Vacuum Relief Valves with integrated Flame Arrester Unit combine two critical safety functions into a single unit: controlled tank breathing and protection against flame transmission.
These valves combine pressure control and explosion protection in a single, type approved device. They prevent atmospheric deflagration and, depending on the design, also protect against endurance burning. This ensures that both operational integrity and safety risks are addressed by one device which provides a durable and easy to maintain solution. In addition these valves reduce emissions and prevent unnecessary air intake. This supports product conservation and stable operating conditions.
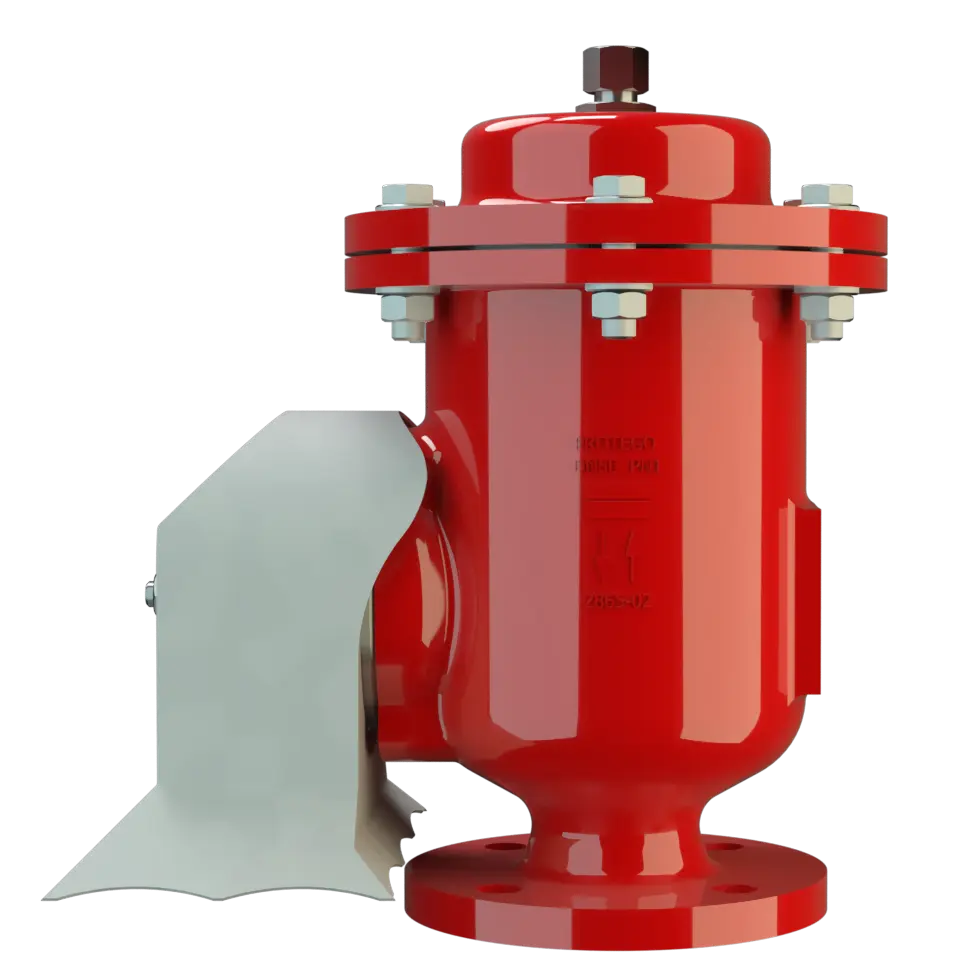
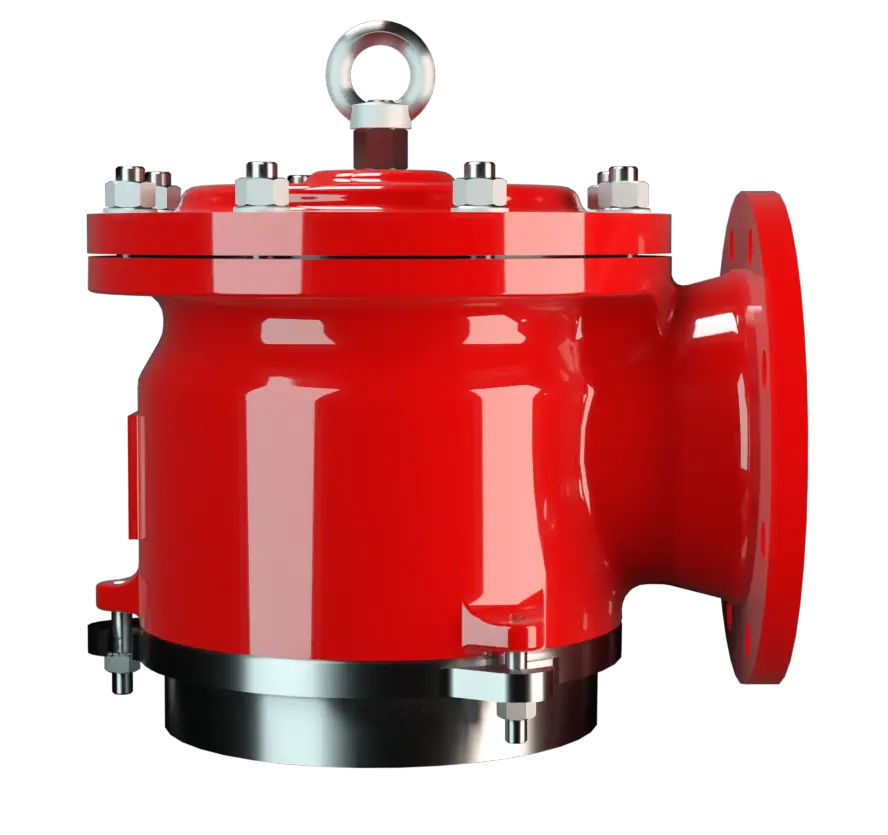
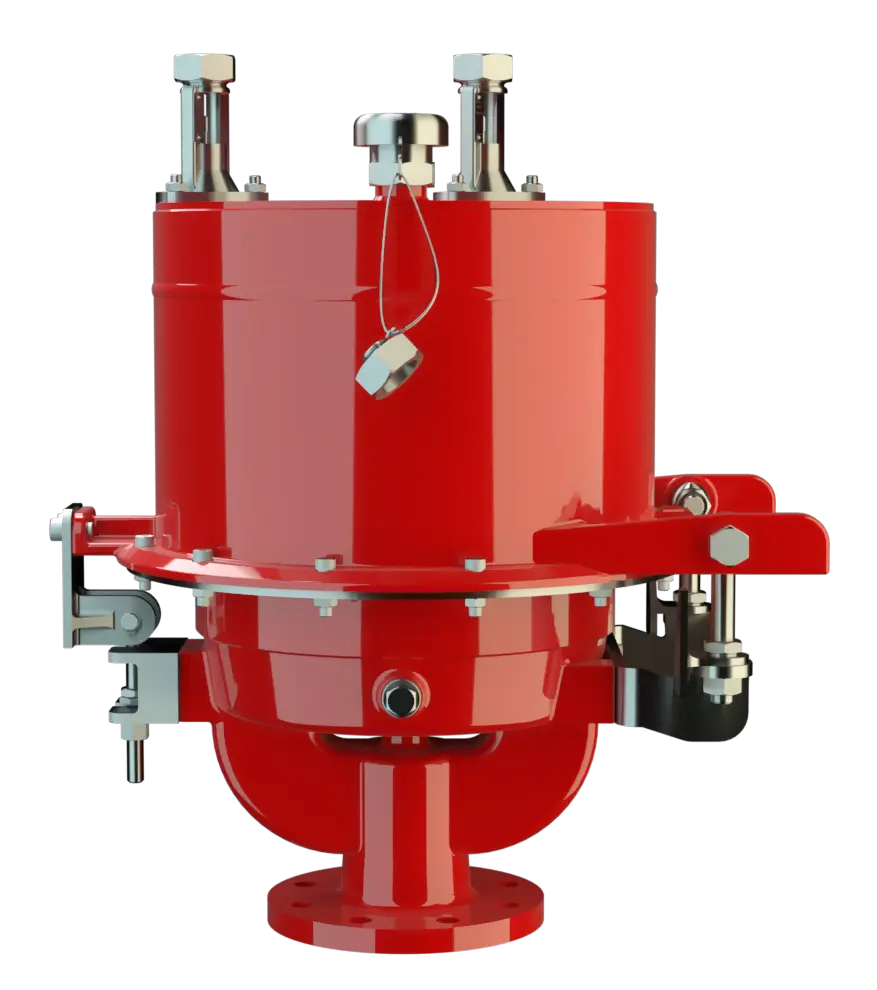
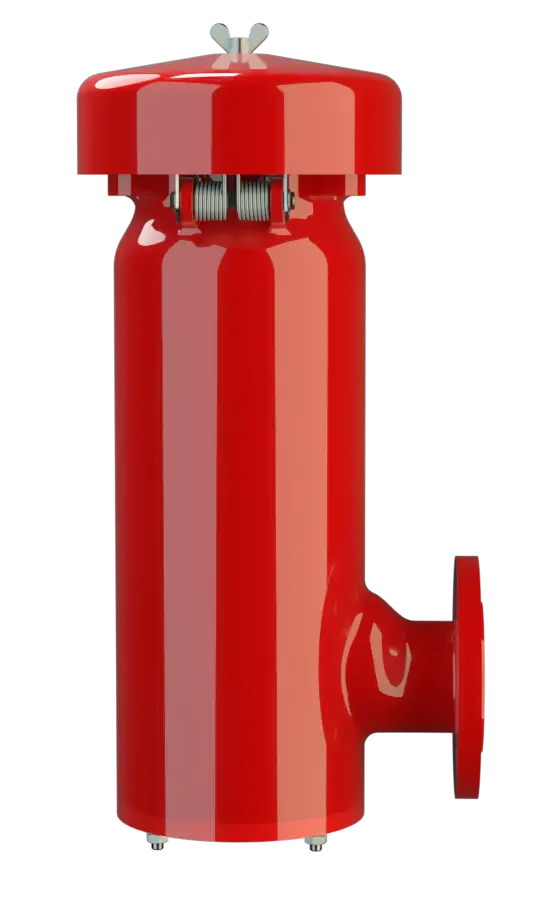
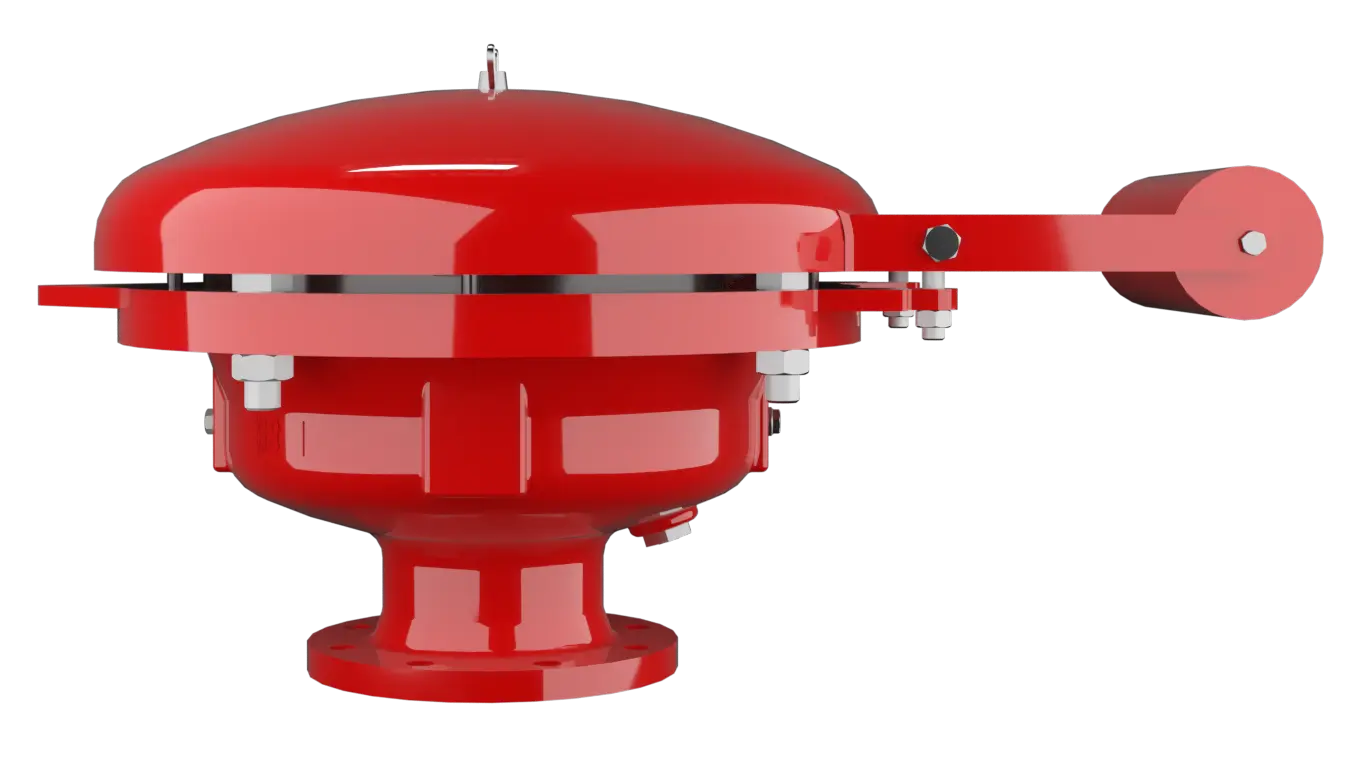
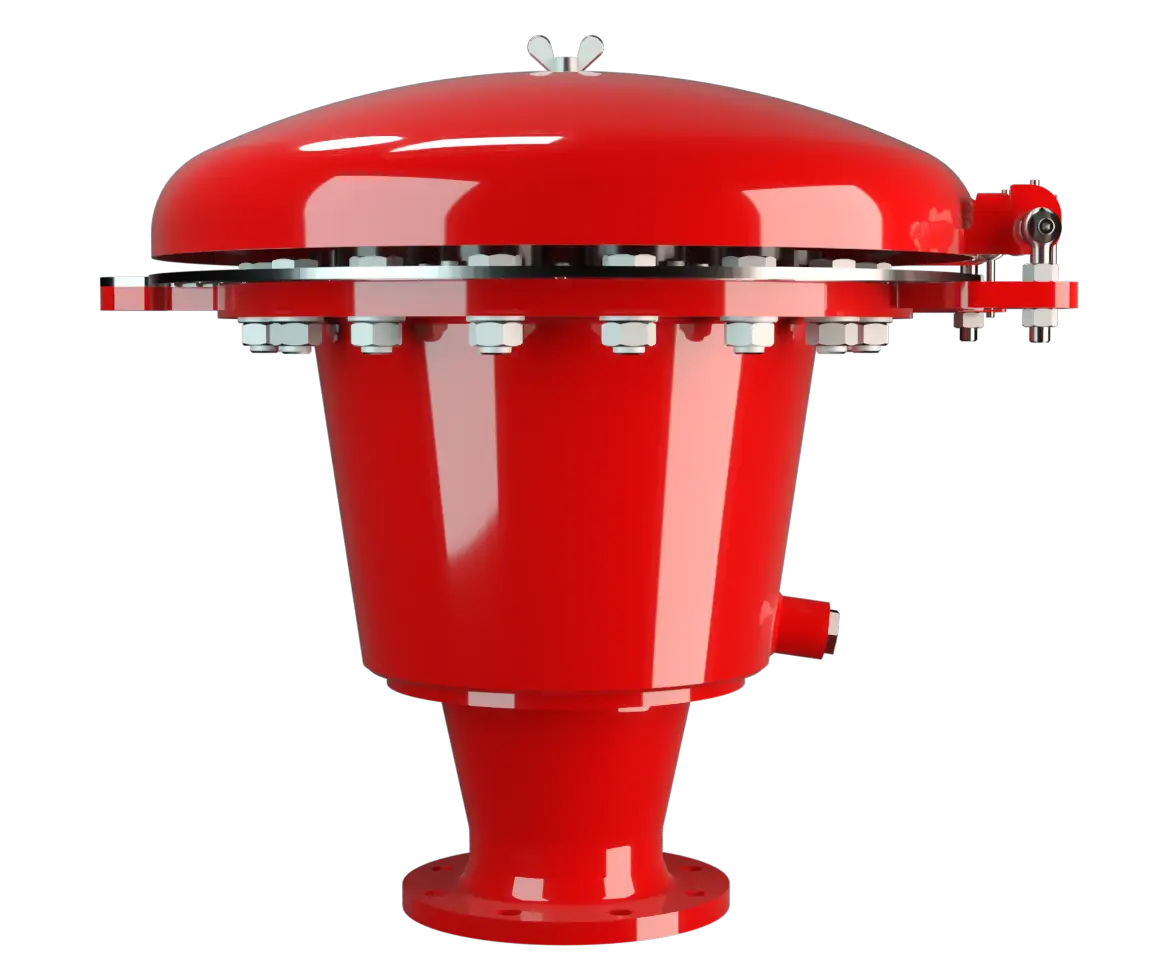
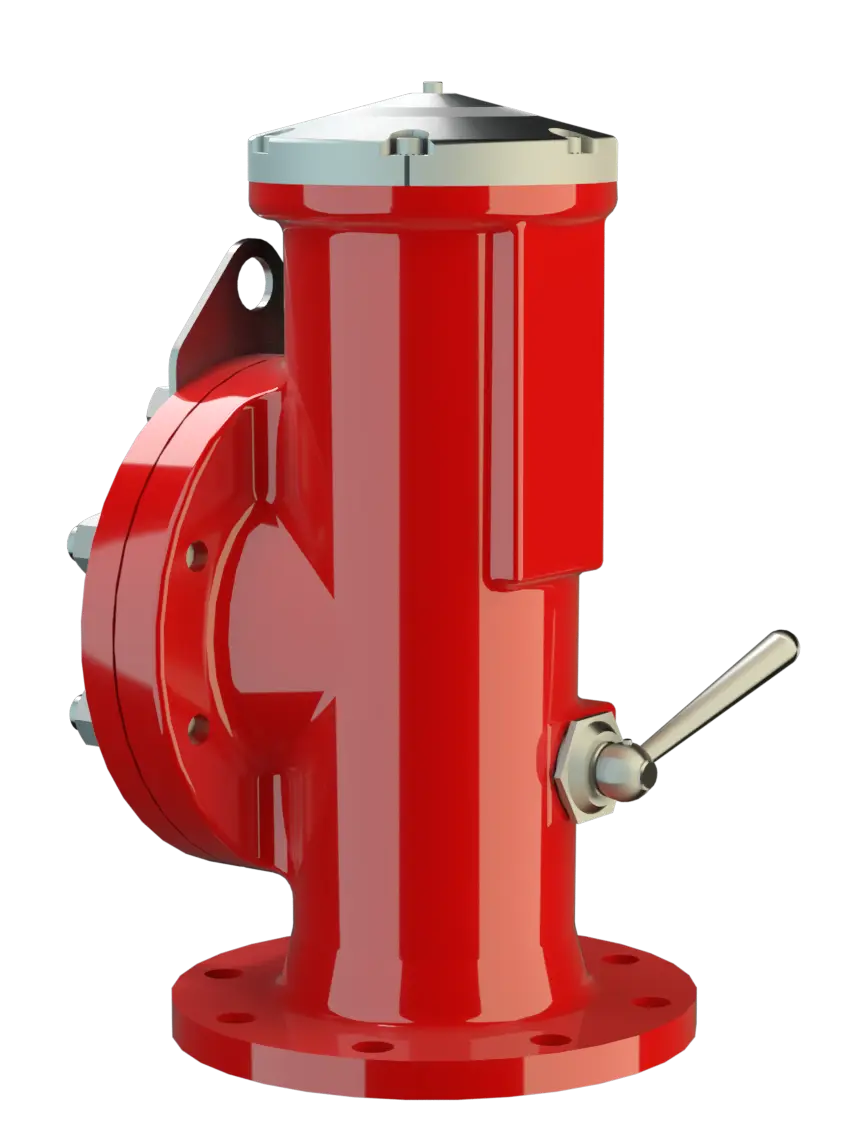
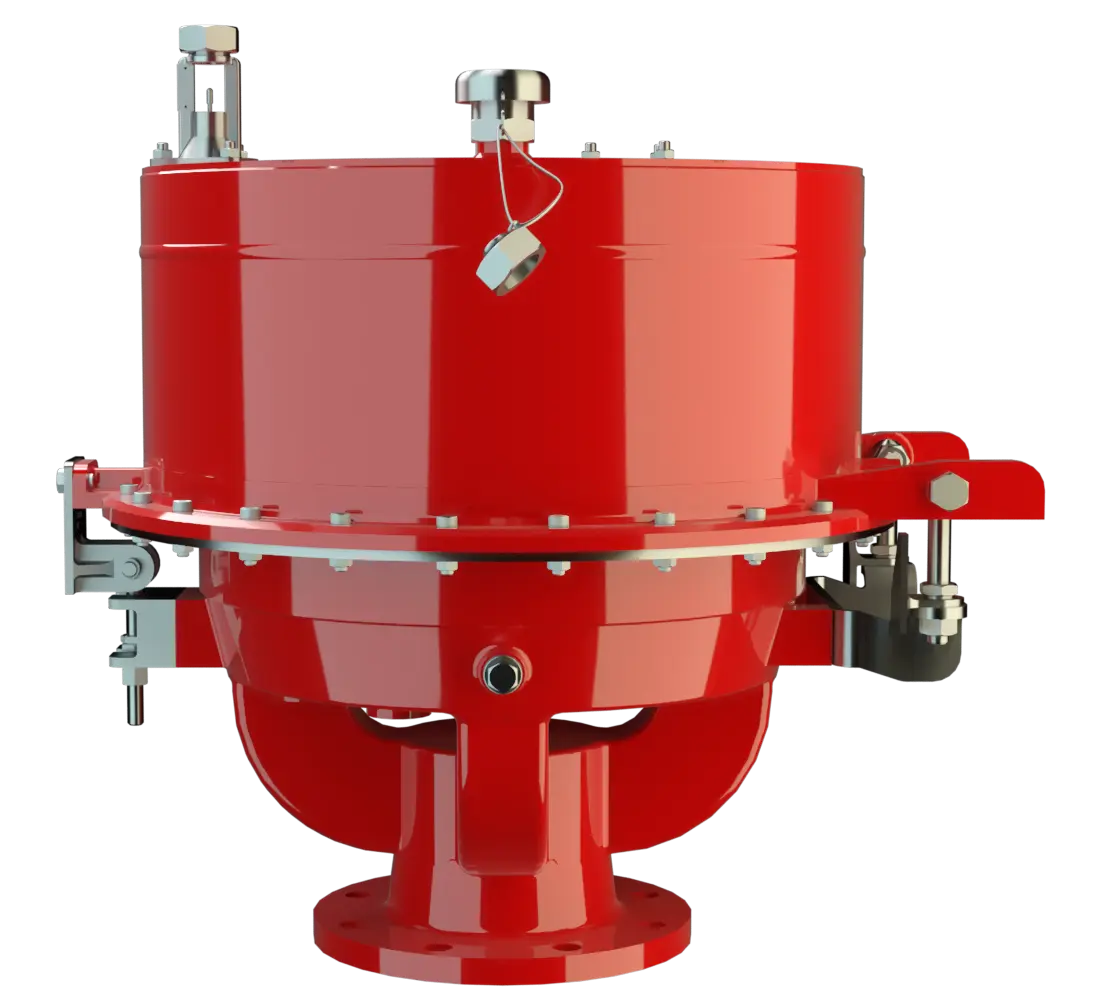
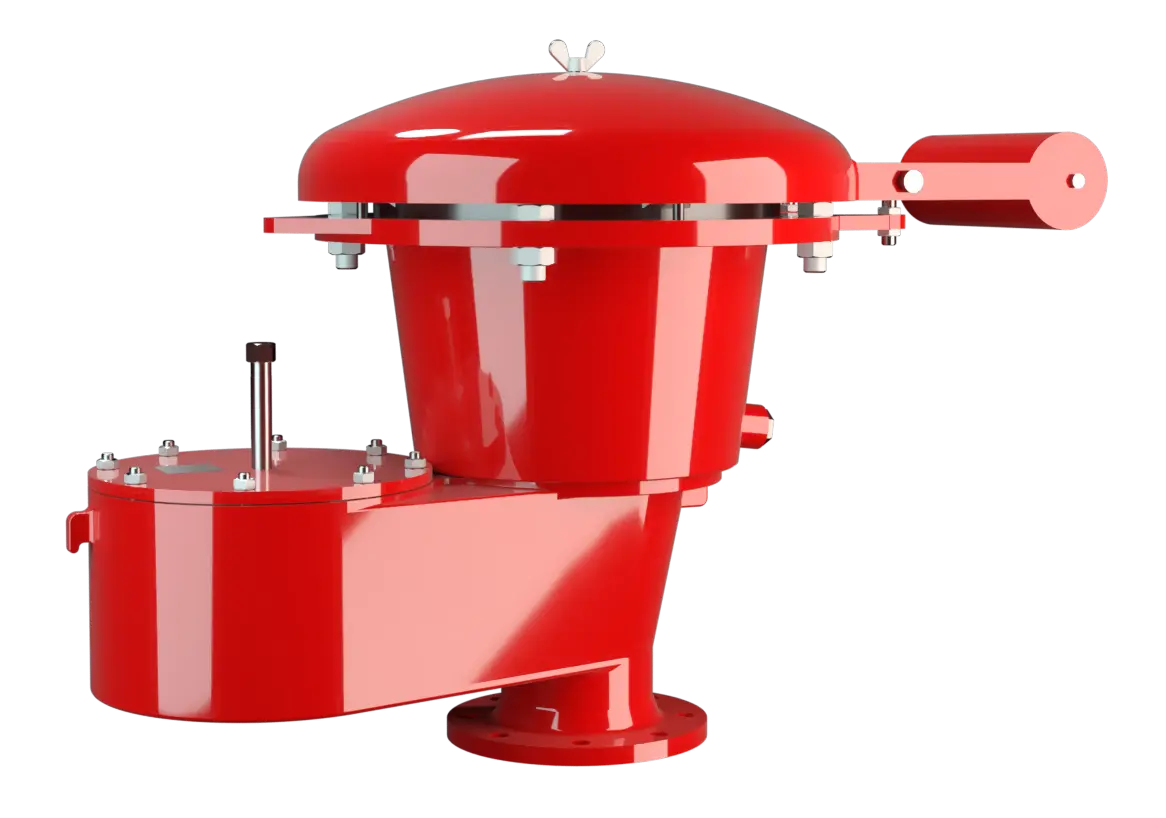
Highlights of PROTEGO® Breather Valves
Zero flashback incidents
How It Works
PROTEGO® Valves use a full-lift-type technology. The valve reaches full lift at 10% accumulation above the set pressure. This allows the valve to deliver full relieving capacity quickly, ensuring that required mass flow is safely discharged before pressure limits are exceeded.
Conventional low-pressure valves require 80% to 100% overpressure to reach full lift. These open earlier and close later, which increases product losses. In contrast, PROTEGO® Valves open later and re-seat earlier. This improves pressure control and reduces unnecessary vapor release.
PROTEGO® Valve and Flame Arrester performance is assured for all relief and explosion scenarios defined in the design case. The pressure drop of the combined device (Flame Arrester and Pressure/Vacuum Valve) is determined on a TÜV-certified flow test rig according to API 2000. The entire device is type approved to ATEX or other relevant international standards for the determined explosion scenarios.
The units are extremely maintenance-friendly and have very low leak rates to reduce explosion risk and ensure compliance with environmental requirements.

The devices have performed as promised with low leak rates and minimal maintenance effort. We highly recommend them.
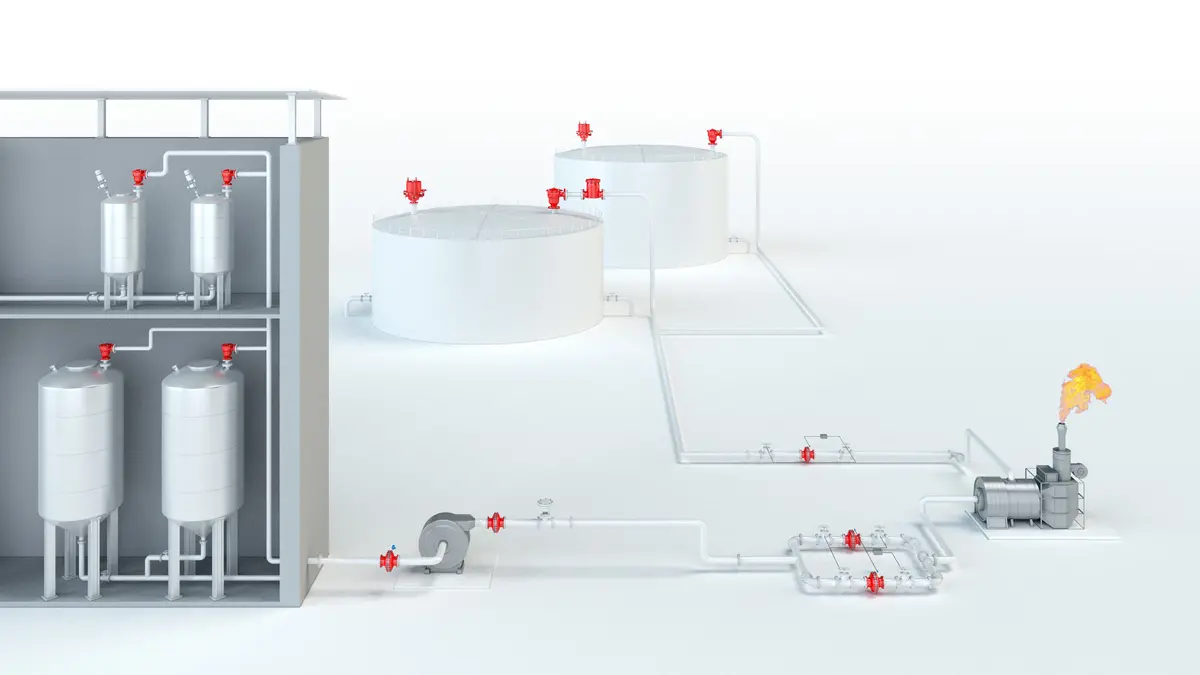
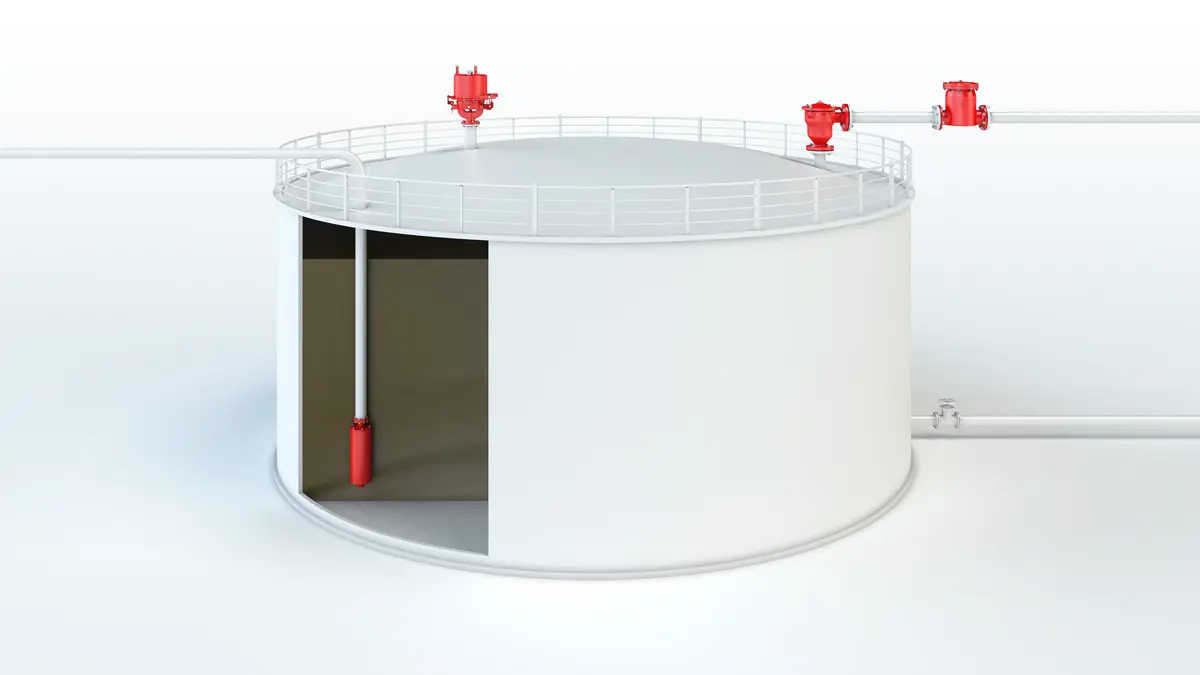
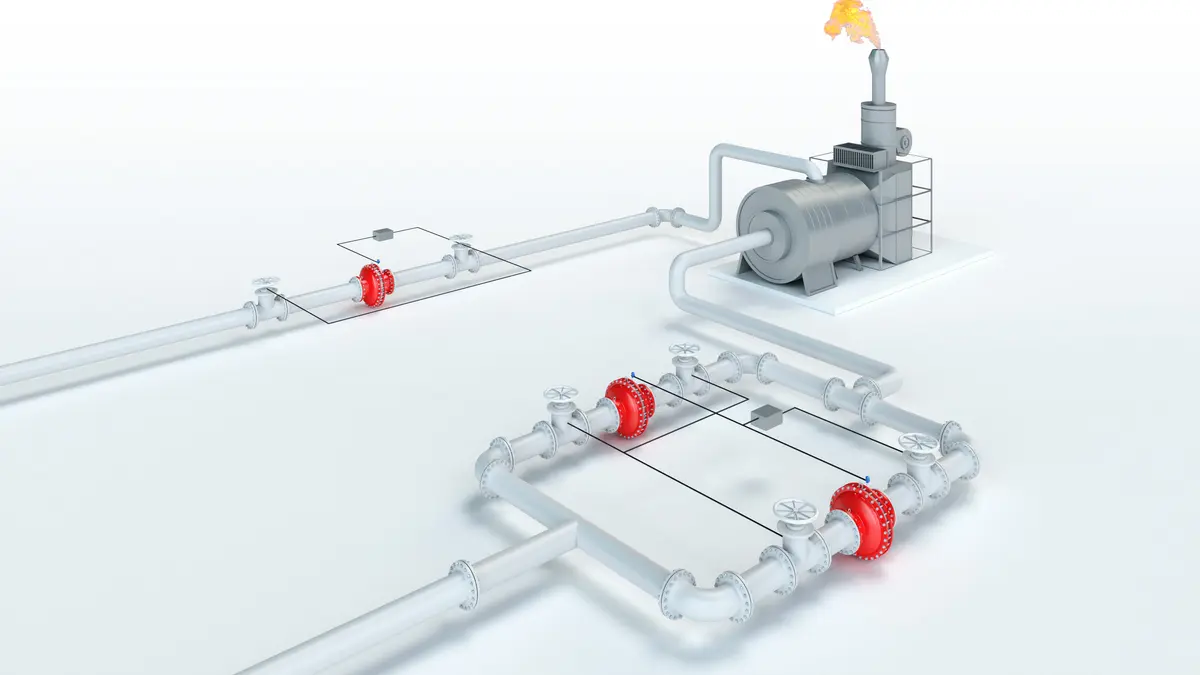
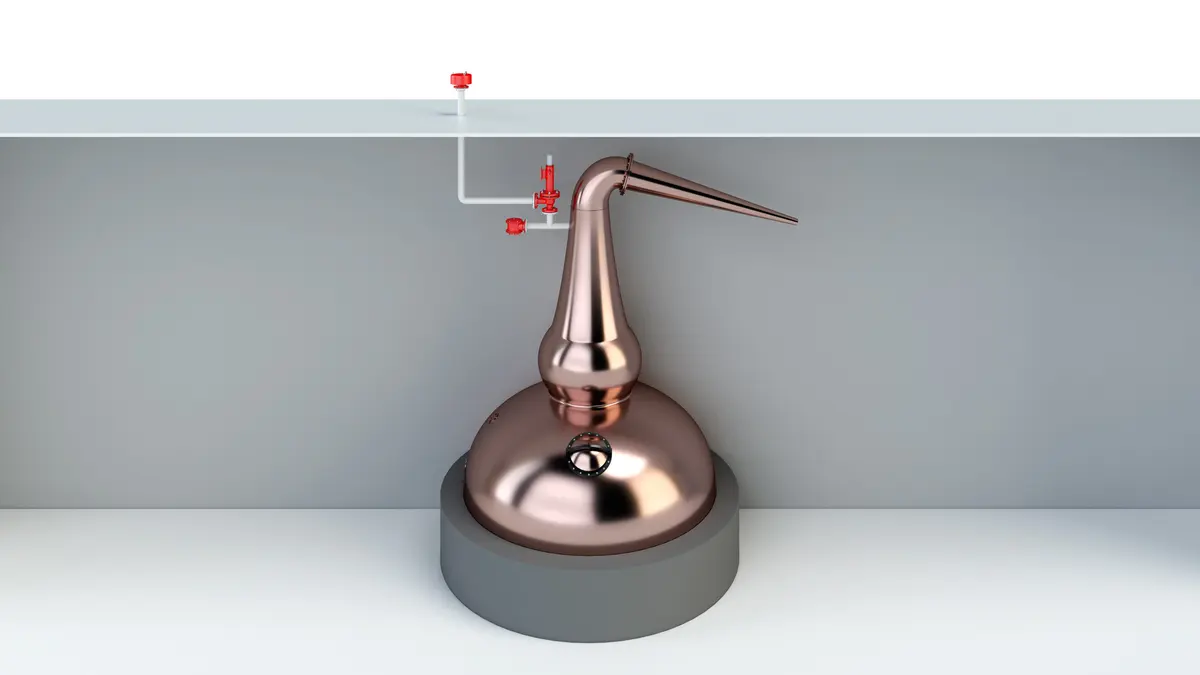
We provide engineered safety solutions.
Since 1954, PROTEGO® has built and provided Flame Arresters, Pressure and Vacuum Relief Valves and Tank Equipment, now with the help of more than 750 employees worldwide.

Engineering and Compliance
Correct valve selection is critical for safe and effective operation. Key selection criteria include:
Valve sizing is based on required volume flow and maximum allowable pressure. Certified volume flow diagrams are available to support design.
Material selection must follow plant and engineering specifications. Options such as metallic or soft sealing are selected based on operating conditions.
Key Features and Design Characteristics
Pressure drop is determined on TUV certified flow test rig according to API 2000 requirements for the combined device (Flame Arrester and Pressure Vacuum Valve).
The valve reaches full lift at 10% overpressure above the set pressure. This allows set pressures to be defined at 10% below the maximum allowable working pressure of the tank. This improves utilization of allowable pressure limits and reduces product losses.
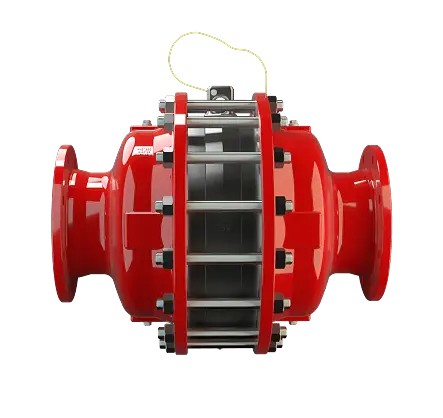
The built-in flame arrester protects against atmospheric deflagration and, in some designs, endurance burning. This ensures that ignition from external sources does not propagate into the system. For in-line valves connected to a vent header combination valve - detonation arresters are type approved to ATEX or other international standards.
The valve reduces emissions almost up to the set pressure. This limits vapor losses during normal operation and supports conservation of stored products.
High flow capacity allows required volume flow to be handled with smaller valve sizes. This reduces equipment size and associated costs.
The valve pallet is guided inside the housing. This protects the moving components from harsh weather conditions and supports reliable operation.
The flame arrester is isolated from the product when the valve is closed. This reduces contamination and extends maintenance intervals.